What Forces a Substrate Change
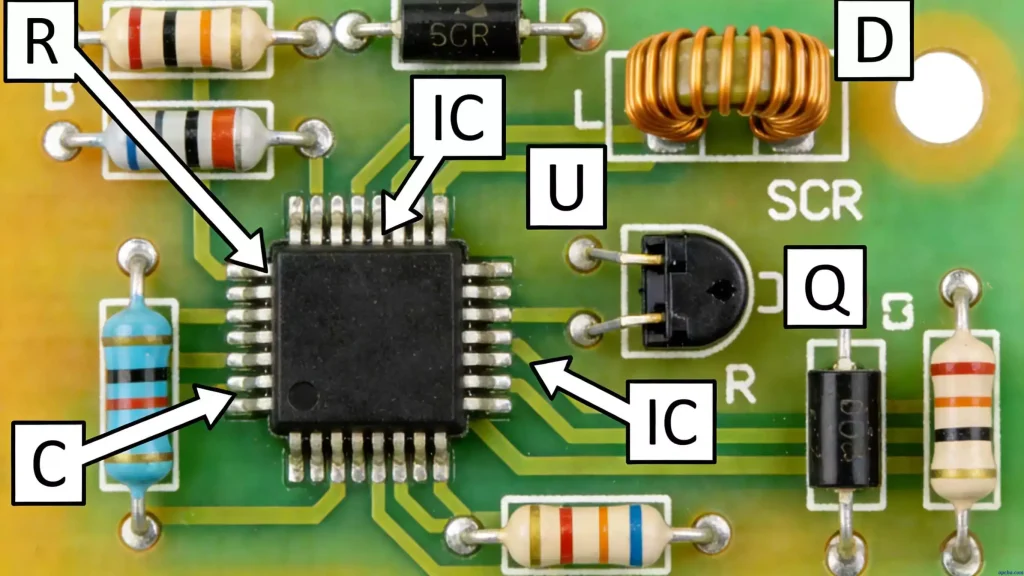
The first visible-light LED reached the market in 1962. It gave off a dim red glow at a few milliamps, and the board underneath it hardly mattered. A plain phenolic laminate carried the current without warming up.
A lighting LED today can pull several watts and concentrate that heat into a few square millimeters of die. At that point the PCB substrate stops being packaging and becomes the part that decides how long the product lasts.
Two bottlenecks sit behind every material upgrade. At low drive currents the limit is copper: whether the traces and planes carry the current without excessive voltage drop. As power climbs, the limit moves to the dielectric: whether heat can cross the insulating layer and reach a metal base or heat sink.
A design that works at 20 mA can fail at 1 A on the same board. The substrate family that suits one LED product is often the wrong choice for the next.
Generation 1: Phenolic and Paper-Based Laminates
Indicator LEDs drew a few milliamps and dissipated milliwatts. Paper-based phenolic laminates, already standard in consumer electronics, handled the current and the heat without modification. They were cheap to punch and drill, and no thermal path design was required.
These materials have not disappeared. They remain in indicator work, where lifespan expectations are modest and performance is not critical, and they were never intended for illumination.
Generation 2: Composite Epoxy Laminates (CEM-1 and CEM-3)
Through the 1970s and 1980s LEDs spread into calculators, clocks, and instrument panels. Volumes rose, and manufacturers wanted a laminate that punched cleanly and cost less than full glass fabric.
Composite laminates filled that gap. They pair a woven glass core with non-woven glass surfacing, or a paper core with a glass surface, which delivers enough mechanical stability at a lower price. CEM-3 still shows up in low-power LED lighting where cost carries more weight than thermal headroom. Its heat path beats paper-based laminate and stays well behind any metal core, which is why it never moved into high-power fixtures. For the material side of that grade, see what CEM3 brings to an LED board.
Generation 3: The Blue LED Turns Lighting into a Thermal Problem
High-brightness blue LEDs, demonstrated in the early 1990s, made white light practical. Coat a blue die with a phosphor and the output reads as white. The three researchers behind the work received the 2014 Nobel Prize in Physics.
With white light available, LEDs left the indicator business and entered general illumination. Drive currents climbed, packages grew, and heat stopped being a rounding error. FR-4, with a thermal conductivity around 0.3 W/m·K, became the limiting component. Heavier copper helped at the trace level but could not move heat through the laminate at the rate a lighting fixture demanded, and the gap widened as power rose. The trade-offs between grades are laid out in this comparison of PCB materials for LED lighting.
Generation 4: Metal-Clad and Insulated Metal Substrates
The answer was to put a metal base under the circuit. A typical metal-clad PCB stacks three layers: an etched copper circuit, a thermally conductive dielectric, and an aluminum base. The LED solders to the white circuit side, and the aluminum back face couples to a heat sink.
The dielectric limits how well the board performs. It has to hold off the working voltage while passing heat, and its thermal resistance usually dominates the whole path from die to ambient. Suppliers have spent decades thinning it without losing breakdown strength, which is the main reason today’s metal-clad PCBs outperform the early ones at the same thickness. The structure and the design details behind it are covered in this guide to aluminum substrates for LED lighting.
Generation 5: Heavy Copper, Copper Cores, and Thermal Separation
Metal-clad PCBs solved conduction, though high-current products exposed a second problem: the copper itself. Street lights and industrial fixtures run multiple LED strings at high drive currents, and thin foil loses current capacity and overheats at the joints.
Designers moved to heavy copper builds, where foil weight sits well above the standard 1 oz, and in some designs to a copper core in place of aluminum. Copper spreads heat laterally better than aluminum and carries more current, at a higher material cost and a weight penalty that matters on suspended fixtures.
Thermal separation arrived alongside it. It routes heat through copper pillars or vias straight from the LED pad to the metal base, bypassing the polymer dielectric. The dielectric still provides electrical isolation, but it no longer sits in the hottest section of the path.
Generation 6: Ceramic Substrates and Embedded Dies
Ceramic boards cover the top end. Alumina and aluminum nitride handle power levels and operating temperatures that metal-clad PCBs cannot reach, and their thermal expansion tracks LED chip materials closely enough to survive repeated thermal cycling. Aluminum nitride reaches thermal conductivity far above any polymer dielectric, in the range of 200 W/m·K, which is why ceramic appears above roughly 20 W or 250 °C of operating temperature and stays out of everything else on cost grounds.
Embedded designs changed where the die sits. Manufacturers machine cavities into the stackup and seat the LED inside them, so the thermal path runs through less material and the finished assembly is thinner. The approach found early traction in backlit interfaces, membrane panels, and compact control assemblies, where space runs out before thermal budget does. We cover that branch in our work on embedded LED PCB design.
What Still Limits LED Substrates
Power density keeps rising, and every increase pushes the same three limits: how thin the dielectric can get before isolation fails, how much copper the design can afford, and how close the die can sit to the metal beneath it.
Two other constraints matter as well. Halogen-free and lead-free requirements narrow the material set available to designers. And as fixtures get thinner, each board has to dissipate more heat from less area, which favors embedded and direct-path approaches over surface mounting.
Choosing a Generation for Your Product
A roadside luminaire, a backlit control panel, and a surgical light sit in different generations, and the cost gap between them is real. Specifying one generation higher than the application needs adds material cost without adding field life.
At OPCBA we build across these substrate families, from standard FR-4 lighting boards through metal-clad and heavy copper to ceramic. Send us your power budget, mechanical envelope, and target life, and we will tell you which generation the design belongs in. Browse our custom LED PCB range for the starting point on stackup and copper weight.