A PCBA solution isn’t just a stack of Gerber files and a BOM. It’s the design, the sourcing, the assembly, and the debugging that turn a block diagram into a box of working boards. Over the years, I’ve seen how easily a small oversight in early planning can cascade into a line-down situation during production. This guide unpacks the stages, the gotchas, and the way we approach it at OPCBA.
What a PCBA Solution Actually Covers
When someone talks about PCBA solutions, they mean the full chain: understanding what the product does, selecting the right components, laying out the board, fabricating it, populating it, and verifying the result. The goal is a board that passes functional test on the first pass, not the third.
Where the Development Process Starts (And Often Stumbles)
Before a single component is placed, we sit down with the customer and define the real requirements. That means more than just a schematic. It means asking about operating temperatures, regulatory standards, whether the product will live outdoors or in an air-conditioned lab. I once had a project where the design assumed a constant 25°C environment; the first prototype shut down at 60°C in the field because no one had talked about the enclosure. That conversation saves months.
Once the requirements are solid, the principle design phase picks the core chips and maps out the functional blocks. Here, a PCBA solution development team looks beyond the datasheet to supply chain reality. Is that microcontroller available in volume? Is the footprint compatible with a second source? These questions shape what gets drawn.
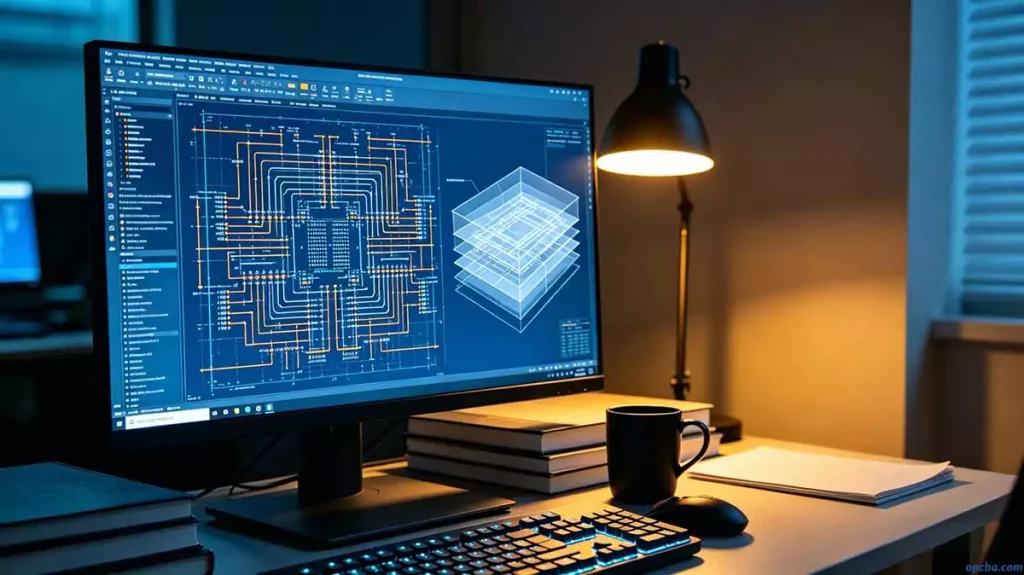
Then comes PCB layout. This is where signal integrity, thermal paths, and electromagnetic compatibility become real. We determine stackup, trace widths, layer counts, and copper weights based on the mechanical constraints and the electrical demands. I’ve learned that rushing into routing without a rigorous stackup review creates impedance mismatches that are a nightmare to debug later.
If you want to dig deeper into the layout rules and techniques that make a board manufacturable and reliable, our PCB Design guide walks through the practical steps and decisions involved.
Component Sourcing: The Unseen Half of the Battle
The most beautifully laid-out board means nothing if the parts can’t be procured. Our PCBA solution development team works closely with suppliers to lock in lead times, verify authenticity, and cross-check specifications. We’ve pulled the plug on a design at the review stage because a key connector was marked “end-of-life” six months prior. Catching that early avoided a costly redesign.
From Bare Board to Assembly Line
PCBA assembly uses SMT and sometimes through-hole processes depending on the mix. The boards go through solder paste printing, automated pick-and-place, reflow, and then inspection. For mixed-technology boards, the DIP section follows. I’m a firm believer in first-article inspection and SPI data trending. Without that, a single clogged stencil aperture can create hundreds of open joints before anyone notices.
Testing: The Stage Where “Working” Is Verified
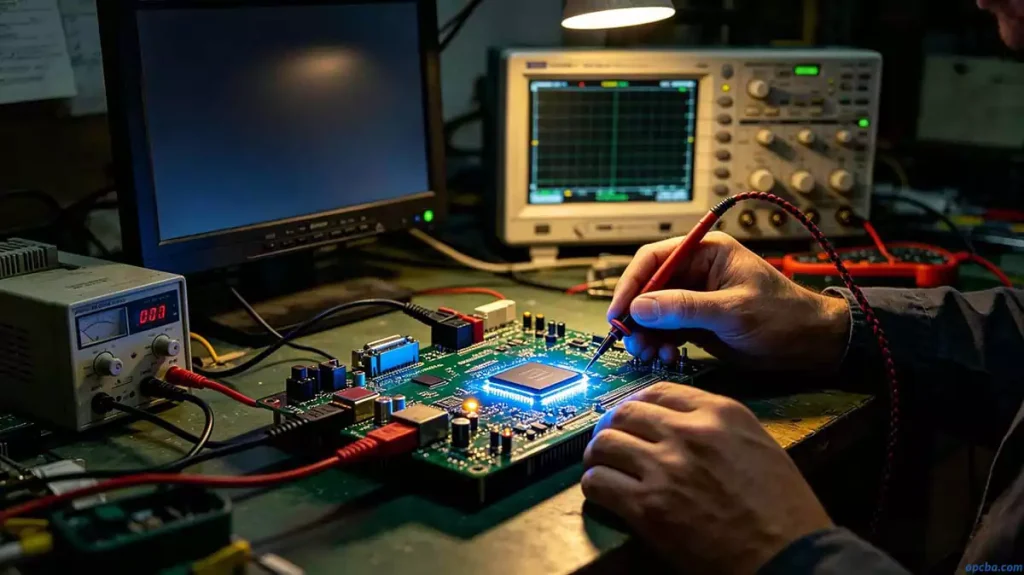
After assembly, every board undergoes functional testing. This isn’t just a power-on check. We verify voltage rails, signal outputs, and key waveforms against the specification. Thermal imaging under load often reveals hotspots that simulation missed. From there, debugging and optimization tighten the performance margins. I’ve seen a simple ferrite bead placement change reduce radiated emissions by 10 dB, turning a marginal EMC test into a clean pass.
The Team and Tools Behind Reliable PCBA
A solid PCBA solution needs an interdisciplinary team: electronic engineers who understand analog and digital design, layout specialists who know DFM, and process engineers who run the SMT line. Tools matter too: precise solder paste inspection and automated optical inspection aren’t luxuries; they’re standard equipment for repeatable quality. Supply chain management ties it all together, ensuring components arrive on time and pass incoming inspection.
OPCBA’s one-stop service covers this entire spectrum, from initial PCBA solutions development to mass production. If you’re not sure how a one-stop model differs from managing multiple vendors separately, our guide on What is the One Stop PCB Assembly Services? explains the key advantages and what to look for.
One-Stop PCBA Solutions by Industry
The same one-stop flow looks different once an industry standard enters the room. The bottleneck moves. Automotive programs stall on qualification paperwork, medical builds stall on traceability records, and consumer builds stall on cost per unit. Here is where each one actually gets stuck.
Automotive PCBA: Qualification Sets the Schedule
Automotive programs carry their own rulebook. Components need AEC-Q100 or AEC-Q200 qualification, the plant works to IATF 16949, and most customers want a PPAP package before the first shipment leaves. None of that can be added at the end, which is why the BOM review happens before layout rather than after. An automotive grade capacitor costs more and has fewer second sources, and that trade-off has to be settled while the schematic is still open. Under-hood positions run from -40 to 125°C, so parts that look fine on a bench get ruled out early.
Every board also needs lot traceability, because a field return has to trace back to a specific component reel. What one-stop PCBA for automotive changes is the number of handoffs. When design, sourcing, assembly and test sit in one place, the qualification evidence is produced while the work happens instead of being rebuilt from vendor emails six months later.
Industrial PCBA: The Ten-Year Supply Problem
Buyers rarely open with price. They ask whether the same board will still be buildable in ten years, when the equipment sits in a factory and the original chip has gone obsolete.
That question reshapes the project. Lifecycle status gets checked before a part enters the design, last-time-buy quantities are planned early, and any single-source component is flagged. Dust, humidity, vibration and wide temperature swings are the constants, so conformal coating is common and EMC margins get tested under real loads rather than with a bench supply. For an industrial PCBA solution, the value is continuity: the same team sees the board through prototype, pilot run and the fifth production batch, so changes stay visible instead of disappearing between vendors. Our industrial control PCB and PCBA page goes deeper into the technical constraints behind those choices.
Medical PCBA: Records Before Boards
Medical work is documentation heavy. ISO 13485 applies to the process, not only the product, and every process change has to be justified and recorded. Low leakage current and patient isolation drive component selection, and the assembly process often needs validation before it touches production units.
Serialization, component lot records and test data belong in one system. Split them across a fab house, an assembly house and an outside test lab, and rebuilding an audit trail becomes a project of its own. Our medical equipment PCB and PCBA page walks through the design and material rules that apply.
Consumer Electronics PCBA: Cost and Calendar
Consumer projects run on the opposite logic. Cost per unit and time to market decide most of the arguments, and the engineering exists to protect both. Work starts with design for manufacturing: panel utilization, component count, and whether a cheaper package does the same job. Prototype runs move fast, and the first build usually shows where the cost really sits. Volume then rewards whatever was simplified early.
One-stop PCBA for consumer products is less about paperwork and more about not losing days between vendors. A layout change that needs a new stencil, a part swap that needs a feeder reset, a fixture that needs rewiring: each handoff costs calendar time that a single site does not spend. Our consumer electronics PCBA page covers the design side in more depth.
Our experience spans telecom, automotive electronics, industrial control, and home appliances. If you have a product concept and need a partner to handle the board-level design and assembly, reach out. We’ll talk through your requirements and map out a plan that fits. Questions buyers ask most often before a first order, from file formats to NDAs, are answered in our PCB and PCBA FAQ.